Skip to content
Anodizing is one of those finishes that looks easy to choose.
A customer sends me an aluminum enclosure drawing. The surface finish column says “black anodized.” The product looks clean. The cost seems acceptable. The engineer feels safe because anodizing is common. The buyer feels safe because many suppliers recommend it.
I understand that feeling very well.
In my work with custom aluminum enclosures, anodizing is often one of the first surface treatments customers ask about. It gives aluminum a clean look. It improves corrosion resistance. It makes the surface harder. It can also help with electrical insulation. For many electronic enclosures, industrial control boxes, Raspberry Pi style cases, sensor housings, and handheld aluminum shells, anodizing is a good choice.
But here is the part many buyers learn later.
Anodizing is not always the best choice.
Sometimes it increases cost without adding real value. Sometimes it creates problems for grounding. Sometimes it makes tight tolerance parts harder to assemble. Sometimes the color is not as stable as the customer expects. Sometimes a simple powder coating or even a brushed finish would be more practical.
I have seen projects where anodizing worked beautifully. I have also seen projects where the customer chose anodizing because it sounded “premium,” and then the real problem appeared after production: color mismatch, blocked threads, poor electrical contact, or a surface scratch that became too obvious.
For me, the key question is not “Is anodizing good?” The better question is:
Does anodizing match the real use of this aluminum enclosure?
That is the way I look at every enclosure project before I suggest a surface finish.
If the enclosure is for display, anodizing may be great. If it needs strong grounding, it may not be. If the enclosure must match a brand color across many batches, anodizing may be risky. If the customer needs a fast prototype, anodizing may slow the whole project down.
In this article, I will explain when you should not choose anodizing for an aluminum enclosure. I will also compare it with other surface treatments, so you can make a better decision before production starts.
What Is Anodizing and Why Is It Commonly Used?
Before I explain when not to choose anodizing, I need to explain what anodizing actually does.
Anodizing is not paint. It is not powder coating. It is not a layer of plastic on top of aluminum.
It is an electrochemical process. The aluminum part is placed into an acid bath, and electrical current is used to grow a controlled oxide layer on the surface. This oxide layer becomes part of the aluminum surface. It does not sit on top in the same way paint does.
That is why anodized aluminum often feels different. It still feels like metal, but the surface becomes harder and more protected.
For many aluminum enclosures, this is useful.
How the Anodizing Process Works
The basic idea is simple.
Aluminum naturally forms a thin oxide layer when it meets air. Anodizing makes this layer thicker, stronger, and more controlled.
A normal anodizing process usually includes:
| Step | What Happens | Why It Matters |
|---|---|---|
| Cleaning | Oil, dust, and machining residue are removed | The surface must be clean before finishing |
| Etching or pre-treatment | The surface is prepared | It affects final texture and appearance |
| Anodizing | Oxide layer grows on aluminum surface | This creates protection and hardness |
| Coloring | Dye or other coloring method may be used | This gives black, silver, red, blue, or other colors |
| Sealing | Surface pores are closed | This improves corrosion resistance and color stability |
This sounds very controlled, and in many ways it is. But it is still affected by material alloy, surface preparation, bath condition, part shape, and batch control.
This is where many buyers underestimate the process.
Anodizing is not just “send the part out and make it black.” It is a finishing process that needs planning.
Key Advantages of Anodized Aluminum Enclosures
I still recommend anodizing for many aluminum enclosure projects because it has real strengths.
Here are the main benefits:
| Advantage | Why Customers Like It | Typical Use Case |
|---|---|---|
| Corrosion resistance | It helps protect aluminum from oxidation | Outdoor sensors, control boxes, device shells |
| Clean appearance | It gives a professional metal look | Consumer electronics, industrial devices |
| Surface hardness | It resists small scratches better than raw aluminum | Handheld equipment, frequently handled cases |
| Lightweight finish | It does not add a thick coating | Precision aluminum housings |
| Electrical insulation | It can reduce unwanted surface conductivity | Some electronic or safety-related applications |
For example, if a customer wants a black aluminum enclosure for a small electronic device, anodizing can look very nice. The finish is thin. The metal texture remains. The product looks neat and technical.
That is why many engineers like it.
Understanding the Limitations Before Choosing Anodizing
The problem starts when anodizing is treated as a default answer.
It should not be.
A good finish depends on the product’s real job. Does the enclosure need grounding? Will the parts be assembled tightly? Will the color need to match another product line? Will the enclosure face heavy impact? Will the customer reorder the same color every few months?
Those questions matter more than the word “anodized” on a drawing.
For one enclosure project, anodizing may be perfect. For another project with almost the same shape, it may cause trouble.
Here is a simple way I think about it:
| Project Requirement | Is Anodizing Usually Good? | Possible Concern |
|---|---|---|
| Premium metal look | Yes | Color variation between batches |
| Electrical grounding | Not always | Oxide layer is insulating |
| Tight assembly tolerance | Needs care | Surface buildup changes dimensions |
| Low-cost prototype | Not always | Extra process adds cost and time |
| Heavy impact use | Not always | Surface can crack or show marks |
| Strong brand color match | Risky | Color may not be perfectly consistent |
For a real project, I usually do not ask only what finish the customer wants. I ask what the enclosure must survive, what parts it touches, and how it will be assembled. A nice surface can become a bad decision if it fights against the product’s function.
A finish is like a pair of shoes. A leather dress shoe looks sharp in a meeting room. But you would not wear it to carry heavy boxes in a wet warehouse.
The same thinking applies to aluminum enclosures.
When Cost Is the Primary Concern
Cost is not a dirty word.
Many buyers feel shy to say, “Vincent, we need to control the cost.” But in B2B projects, cost is part of the product design. A beautiful enclosure that kills the customer’s margin is not a successful enclosure.
Anodizing often costs more than a very simple raw, brushed, or basic surface finish. It may also cost more when the quantity is small, the part shape is complex, or the color control requirement is high.
This does not mean anodizing is expensive in every case. It means the buyer should check whether the added cost brings real value.
Anodizing Can Increase Manufacturing Costs
Anodizing adds extra steps after machining, cutting, bending, drilling, or CNC processing.
The part must be cleaned. It must be handled carefully. It must be sent to the anodizing line. It must be inspected again after finishing. If the color is not right, the supplier may need to remake or refinish the part.
That extra work has a cost.
For small-batch aluminum enclosures, this becomes more obvious. If the order is only 20 pieces, 50 pieces, or a prototype batch, the finishing cost per unit may be higher than expected.
Here is a simple example:
| Project Type | Anodizing Impact | Why It Matters |
|---|---|---|
| Prototype sample | Higher unit cost | Setup and handling cost is spread over few parts |
| Small batch | Medium to high cost impact | Minimum finishing charge may apply |
| Large production | More acceptable | Cost is spread across more units |
| Complex enclosure | Higher risk and cost | More holes, corners, and surfaces need control |
| Strict cosmetic part | Higher inspection cost | More parts may fail visual standards |
In my work, I sometimes see customers choose anodizing because they want the product to look professional in the first sample. That makes sense if the sample is for investor review, trade show display, or customer approval.
But if the sample is only for internal testing, anodizing may be unnecessary at that stage.
One buyer once pushed for black anodizing on an early enclosure prototype. The design changed twice after the first test. The mounting holes moved. The side cutout changed. The logo position changed. The anodized sample looked nice, but it was already outdated after one meeting.
That is a painful way to spend money.
More Economical Alternatives
If cost is the first concern, there are several alternatives.
They are not always better. But they may be better for the right project.
| Finish Option | Cost Level | Best For | Limitation |
|---|---|---|---|
| Raw aluminum | Low | Internal prototype, test fitting | Poor cosmetic appearance, easier oxidation |
| Brushed aluminum | Low to medium | Simple industrial look | Less corrosion protection than anodizing |
| Sandblasting only | Low to medium | Matte texture, sample parts | Needs protection for long-term use |
| Powder coating | Medium | Strong color coverage, brand color | Thicker coating, affects tolerance |
| Painting | Medium | Custom colors, cosmetic parts | Can chip if not controlled well |
If the enclosure is hidden inside a machine, the surface may not need a premium anodized look.
If the product is a temporary test unit, raw aluminum may be enough.
If the customer wants a matte black enclosure but also wants lower cost and better color coverage, powder coating may be a better option.
How to Evaluate Cost vs. Performance
I like to compare cost with actual product value.
Not every product needs the same finish level.
Ask these questions:
- Will the customer see the enclosure every day?
- Will the enclosure be touched often?
- Will it be used indoors or outdoors?
- Is corrosion resistance critical?
- Is the product a prototype or final production?
- Does the finish help the customer sell the product?
- Does the finish protect the product in real use?
Here is how I usually judge it:
| Situation | My Suggestion |
|---|---|
| Internal engineering sample | Avoid anodizing unless testing surface fit |
| Trade show sample | Consider anodizing if appearance matters |
| Indoor control box | Use anodizing only if the customer needs it |
| Premium electronic device | Anodizing may be worth the cost |
| Hidden machine part | A simpler finish may be enough |
| Low-margin wholesale product | Compare powder coating or brushed finish |
The small detail I check is whether the surface finish helps the customer make money or avoid failure. If it only makes the drawing look more “complete,” I usually suggest saving the cost for better structure, packaging, or faster delivery.
That is not because anodizing is bad.
It is because every dollar in a custom enclosure project should have a job.
And sometimes anodizing is just standing there wearing a suit at a barbecue.
When Your Enclosure Requires Electrical Conductivity
This is one of the most important reasons not to choose anodizing.
Anodizing creates an oxide layer on the aluminum surface. That oxide layer is protective, but it is also electrically insulating.
For some products, that is fine. For other products, it creates real problems.
If the aluminum enclosure must act as part of the grounding path, or if it must help with EMI shielding, anodizing needs careful planning.
Anodizing Creates an Insulating Surface
Many people think aluminum is conductive, so an aluminum enclosure must always conduct electricity well.
The base aluminum is conductive. But the anodized surface is different.
The anodized oxide layer can reduce electrical contact between:
- Cover and base
- Panel and chassis
- Screw and enclosure body
- PCB ground point and metal housing
- Connector shell and enclosure wall
This can create trouble when the design depends on metal-to-metal contact.
A screw may look tight. A panel may look assembled. But the electrical path may not be good enough.
That is the kind of problem that does not always appear in photos. It appears during testing.
Problems for Grounding and EMI Shielding Applications
For electronic enclosures, grounding is not a small detail.
A product may need grounding for safety. It may need shielding to reduce electromagnetic noise. It may need clean contact between the connector and the enclosure. It may need stable performance in industrial environments.
If anodizing covers all contact areas, the enclosure may not provide the expected electrical path.
Here is a common issue:
| Design Area | Possible Problem After Anodizing |
|---|---|
| Screw holes | Screws may not make strong electrical contact |
| Internal grounding points | PCB ground may not connect well to housing |
| Panel joints | EMI shielding may be reduced |
| Connector openings | Connector shell may not bond to enclosure |
| Hinges or covers | Contact may be inconsistent |
For example, a customer may design an aluminum enclosure for a communication device. The product needs shielding. The engineer chooses black anodizing because the product also needs a clean appearance. After assembly, the enclosure looks perfect. But the test shows poor grounding between the cover and the base.
Now the team has to remove anodizing from some areas, add conductive gaskets, or change the finishing plan.
That is extra time. Extra cost. Extra stress.
Better Surface Treatment Options
If electrical conductivity matters, anodizing may still be possible, but not on every surface.
There are several options:
| Solution | How It Helps | What to Watch |
|---|---|---|
| Masking before anodizing | Keeps selected areas bare | Needs clear drawing and good process control |
| Post-machining contact areas | Removes anodizing from grounding points | Adds extra machining step |
| Conductive gasket | Improves EMI contact between parts | Adds material cost |
| Chromate conversion coating | Offers corrosion resistance with better conductivity | Appearance may not be as decorative |
| Bare aluminum contact points | Simple and effective | Needs corrosion control |
| Conductive coating | Helps special EMI requirements | Cost and supplier capability matter |
The mistake I try to avoid is treating conductivity as something we can fix at the end. If grounding is important, I want to discuss contact areas before finishing, because after anodizing, every small contact point becomes a negotiation with the surface.
A good engineering drawing should not only say “black anodized.”
It should also show:
- Which areas need electrical contact
- Which areas should be masked
- Which holes must remain conductive
- Which surfaces need cosmetic quality
- Which surfaces are hidden and can be treated differently
This is why I ask questions that may sound small at first.
“Does this screw need to conduct?”
“Does the connector shell need grounding?”
“Will the lid contact the base for EMI shielding?”
These questions can save the project later.
A pretty enclosure with poor grounding is like a nice-looking umbrella with tiny holes. It may look fine until the rain starts.
When Tight Dimensional Tolerances Are Critical
Anodizing changes the surface of the aluminum part.
The change is small. But in precision enclosure projects, small changes matter.
If the enclosure has tight sliding parts, threaded holes, press-fit components, or precision mating surfaces, anodizing must be considered during design.
Anodizing Changes Surface Dimensions
Anodizing creates an oxide layer. Part of the oxide grows into the aluminum surface, and part grows outward.
This means the final dimensions may change slightly.
For a large cover plate, this may not matter.
For a tight groove, threaded hole, or precision slot, it can matter a lot.
A small dimensional change can cause:
- Screws not fitting smoothly
- Sliding covers becoming too tight
- Press-fit parts failing
- PCB mounting issues
- Gaps between mating parts
- Assembly time increasing
Here is a simple view:
| Feature | Why Anodizing Can Be a Problem |
|---|---|
| Threaded holes | Coating may reduce thread clearance |
| Sliding rails | Surface buildup may make movement tight |
| Press-fit bosses | Fit may become too tight after finishing |
| PCB mounting pockets | Board may not sit correctly |
| Connector cutouts | Tight connectors may not fit |
| Cover-to-base joints | Assembly may become harder |
In custom enclosure manufacturing, this is one of those details that separates “looks good on the drawing” from “works well in assembly.”
Common Problem Areas
Threads are a common example.
If a hole is tapped before anodizing, the anodized layer may affect the thread. The screw may still go in, but it may feel rough or tight. In some cases, the screw may damage the anodized layer during assembly.
For precision mating surfaces, the problem may be more subtle.
The parts may fit during the first sample before finishing. Then they become tight after anodizing. The customer may think the machining tolerance is wrong, but the real issue is that the finish was not considered.
This can also happen with aluminum enclosures that have:
- Internal rails for PCB boards
- Snap-fit covers
- Sliding battery covers
- Heat sink contact surfaces
- Internal support ribs
- Connector pockets
- Assembly grooves
A little surface growth can become a big headache when the design has no room to breathe.
Alternative Finishing Methods
There are ways to reduce this risk.
The best method depends on the product design.
| Method | Use Case | Benefit |
|---|---|---|
| Increase tolerance allowance | Parts with mating surfaces | Prevents tight assembly |
| Mask critical areas | Contact or fit areas | Keeps dimensions stable |
| Machine after anodizing | Precision final surfaces | Improves final accuracy |
| Tap after anodizing | Threaded holes | Better screw fit |
| Use powder coating carefully | Cosmetic parts | Good coverage, but thicker than anodizing |
| Leave hidden precision surfaces unfinished | Internal fit areas | Simple and practical |
Of course, every method has trade-offs.
Masking adds process control. Machining after anodizing may expose raw aluminum. Tapping after anodizing adds labor. Powder coating is thicker than anodizing, so it may create even bigger tolerance problems if not planned.
The point is not to avoid anodizing every time.
The point is to design for it.
When I review a tight enclosure design, I look at where hands, screws, boards, and connectors will meet the metal. If those areas are tight on paper, I do not trust luck; I adjust the tolerance or suggest keeping those surfaces unfinished.
That is a very practical habit.
Because in production, a part does not care how beautiful the 3D drawing looked.
It only cares whether the screw can go in.
When Extreme Color Consistency Is Required
Anodizing can look beautiful.
Black anodized aluminum can look clean and professional. Silver anodizing can look modern. Red, blue, gold, or gray anodizing can make a product stand out.
But if your product needs perfect color consistency across different batches, anodizing can be risky.
This is especially true for brand-sensitive products.
Color Variation Can Occur During Anodizing
Anodizing color is affected by many things.
The aluminum alloy matters. The surface preparation matters. The anodizing bath matters. The dye matters. The sealing process matters. Even part geometry can affect the final look.
Two parts may both be “black anodized,” but they may not look exactly the same under the same light.
One may look deep black. Another may look slightly gray. One batch may look warmer. Another batch may look cooler.
That may not matter for industrial equipment.
It may matter a lot for consumer-facing products.
| Factor | Effect on Anodized Color |
|---|---|
| Aluminum alloy | Different alloys absorb dye differently |
| Surface texture | Brushed, blasted, or machined surfaces reflect light differently |
| Batch condition | Bath chemistry can affect final shade |
| Part thickness and shape | Current distribution may vary |
| Sealing process | Can affect final color tone |
| Reorder timing | Later batches may not match earlier batches perfectly |
This is why I am careful when a customer says, “We need the same black as last year.”
I can try to match it. I can use samples. I can control the process. But I should not promise magic.
Challenges for Brand-Sensitive Products
Color consistency becomes more difficult when the enclosure is part of a product family.
For example:
- A customer sells several device models under one brand.
- The front panel and back cover are made in different batches.
- The product is sold online, so photos must look consistent.
- The customer reorders every three months.
- The product sits next to plastic parts, labels, screens, or accessories.
In that case, small color differences become more visible.
The customer may compare the new enclosure with old stock. Their end users may compare two units side by side. Their marketing team may compare the real product with website photos.
That is when “almost the same black” may not be good enough.
I have seen buyers feel surprised by this. They expected anodizing to behave like paint. But anodizing is not paint. It is more connected to the metal surface itself.
Better Choices for Consistent Appearance
If the main goal is strict color matching, powder coating or painting may be better.
These methods sit on top of the surface. They can be matched more closely to RAL, Pantone, or other color standards.
| Finish | Color Consistency | Best For |
|---|---|---|
| Anodizing | Good, but batch variation possible | Metal look, premium technical appearance |
| Powder coating | Usually better for consistent color | Brand colors, industrial products |
| Wet painting | Flexible color matching | Cosmetic products, small custom colors |
| Silk screen or UV printing | Good for logo and graphic areas | Branding and markings |
| Brushed natural aluminum | Avoids color dye issue | Simple metal look |
If a customer is building a long-term product line, I usually ask whether future repeat orders must match the first order very closely. If the answer is yes, I become more careful with colored anodizing, especially black, gray, red, and gold.
One small thing I like to check is whether the customer will sell replacement parts later. If they will, color difference becomes more painful, because a replacement cover may sit beside an older base and expose the mismatch immediately.
That is the kind of detail buyers often miss at the beginning.
The first order looks fine.
The second order starts the argument.
Color is emotional. Engineers may talk about tolerance, but customers often react to color first.
A slightly different shade can make a good product feel inconsistent.
When Maximum Impact Resistance Is Needed
Anodizing increases surface hardness.
That sounds like it should always improve durability.
But surface hardness and impact resistance are not the same thing.
A hard surface can still show damage when it is hit, dropped, scraped, or bent. In some harsh-use products, anodizing may not be the best finish.
Anodized Layers Can Be Brittle
The anodized layer is hard, but it does not behave like rubber. It does not absorb impact well.
If the aluminum part is hit hard or bent, the anodized surface may crack, chip, or show white marks. Sharp edges are especially vulnerable.
This matters for enclosures used in:
- Industrial workshops
- Outdoor installation
- Field service equipment
- Transportation devices
- Rental equipment
- Tools carried in bags or trucks
- Products handled by many users
A product may survive structurally, but the surface may look damaged quickly.
That can hurt the customer’s brand image.
Risk of Cracking or Chipping
The risk is higher when the enclosure has sharp corners, thin walls, or areas that receive frequent contact.
For example, if an enclosure is mounted on a machine and workers often hit it with tools, anodizing may show wear at the edges. If the enclosure is a handheld device dropped on concrete, corners may become ugly quickly.
Here is a practical comparison:
| Use Condition | Anodizing Risk |
|---|---|
| Light indoor use | Low risk |
| Desktop electronic device | Usually acceptable |
| Handheld field device | Medium risk |
| Heavy industrial use | Higher risk |
| Sharp-edge enclosure | Higher risk at corners |
| Frequent transport | Scratches and edge wear possible |
Some customers choose anodizing because they hear “hard surface.” That is true. But if the product faces impact, I also care about flexibility, coating thickness, edge protection, and repairability.
A hard surface is not always a tough surface.
Glass is hard too. But nobody calls a glass phone screen unbreakable.
Alternative Finishes for Harsh Conditions
For harsh environments, powder coating may be better in many cases.
Powder coating creates a thicker layer. It can cover edges better if designed properly. It also gives strong color coverage. For some industrial enclosures, this is more practical than anodizing.
Plastic enclosures may also be better for impact in some applications, especially when the product needs shock absorption, light weight, or lower cost.
| Finish or Material | Why It May Be Better |
|---|---|
| Powder coating | Thicker protection and better color coverage |
| Textured powder coating | Hides small scratches better |
| Plastic enclosure | Better impact absorption in some designs |
| Rubber corner protectors | Protects drop-sensitive areas |
| Hybrid aluminum + plastic design | Balances strength and impact resistance |
| Hard anodizing | Better wear resistance, but cost and color limits matter |
I pay attention to how the enclosure will be treated after it leaves the factory. A product used by careful engineers in a lab is different from a product thrown into a service van every day.
That difference should guide the finish.
If the product will have a hard life, I would rather choose a surface that forgives abuse.
Because real users do not handle products like sample inspectors.
They drop things. They stack things. They drag things across tables. They put them in bags with tools and cables.
That is real life.
When Rapid Prototyping and Fast Lead Times Matter
Speed matters in custom enclosure projects.
Many customers come to us because they are developing a new product. Their PCB is ready. Their engineer needs a case for testing. Their sales team wants a sample for a customer meeting. Their project schedule is already tight.
In this situation, anodizing may slow things down.
Not always, but often enough that it deserves attention.
Anodizing Adds Additional Production Steps
An aluminum enclosure does not become anodized by itself after machining.
It must go through extra finishing steps.
Those steps include surface cleaning, pre-treatment, anodizing, coloring, sealing, drying, inspection, and packaging protection.
Each step adds time.
If the supplier has an in-house anodizing line, the schedule may be easier to control. If the part must be sent to an outside finishing partner, the lead time may be longer.
Here is a simple view:
| Process Stage | Time Risk |
|---|---|
| CNC machining or sheet metal fabrication | Main production time |
| Surface preparation | Extra handling |
| Anodizing queue | Depends on batch schedule |
| Color approval | May need sample confirmation |
| Inspection | Cosmetic defects may cause rework |
| Packing | Anodized parts need careful protection |
For a standard production order, this may be acceptable.
For an urgent prototype, it may not be.
How It Can Delay Prototype Development
Prototype work is messy.
That is normal.
A prototype is not a final product. Holes move. Cutouts change. Bosses become taller. Wall thickness changes. The customer realizes the cable needs more room. The PCB connector is not where the first drawing said it would be.
If every prototype revision needs anodizing, the schedule becomes slower and more expensive.
For early-stage development, I often suggest making the first sample without anodizing. We can check structure, assembly, PCB fit, connector position, and thermal space first. After the design is stable, we can make a finished sample.
That is usually smarter.
| Prototype Stage | Suggested Finish |
|---|---|
| First structure test | Raw aluminum or simple brushed finish |
| PCB fit test | Raw or light surface treatment |
| Customer demo sample | Anodizing or powder coating may be useful |
| Pre-production sample | Final finish required |
| Mass production | Final approved finish |
This is how I reduce wasted time.
A beautiful prototype with the wrong holes is still the wrong prototype.
Faster Alternatives
If speed is more important than final appearance, there are faster options.
| Alternative | Best Use |
|---|---|
| Raw machined aluminum | Fast fit testing |
| Brushed finish | Simple appearance with less delay |
| Sandblasted surface | Better sample look without full finishing complexity |
| Temporary protective film | Prevents scratches during testing |
| Powder coating | Sometimes faster depending on local supply chain |
| 3D printed or plastic prototype | Early shape verification |
Of course, the right option depends on the project.
If the customer must show the sample to an investor, final appearance matters. If the customer only needs to test PCB fit, anodizing may be a waste of time.
The question I ask myself is whether the customer is testing the enclosure’s function or selling the enclosure’s appearance. If they are still testing function, I try to keep finishing simple until the design stops moving.
That small decision can save one or two rounds of delay.
And in product development, one saved week can feel like oxygen.
When the Product Operates in Highly Visible Cosmetic Applications
This point may sound strange at first.
Anodizing is often chosen because it looks good. So why would I say it may not be suitable for highly visible cosmetic applications?
Because anodizing does not hide surface defects well.
In many cases, it makes them easier to see.
Anodizing Highlights Surface Imperfections
Anodizing follows the aluminum surface.
If the part has tool marks, scratches, dents, material lines, or uneven polishing, anodizing may not cover them. It may even make them more obvious.
Paint and powder coating can hide some small defects because they sit on top of the surface. Anodizing is different. It becomes part of the surface.
That means the original metal condition is very important.
Common visible issues include:
- CNC tool marks
- Extrusion lines
- Scratches from handling
- Uneven brushing
- Weld marks
- Material grain differences
- Fingerprint-like stains before finishing
- Sharp edge color differences
If the customer expects a luxury cosmetic surface, anodizing requires very careful pre-treatment.
That adds cost and inspection work.
Why Cosmetic Quality Becomes More Difficult
Cosmetic quality is not only about the finishing process.
It starts much earlier.
It starts with material selection, cutting, machining, deburring, polishing, handling, cleaning, and packaging.
If one step is careless, anodizing may reveal the problem.
Here is a simple chain:
| Step | Risk Before Anodizing |
|---|---|
| Material purchase | Alloy or surface quality may vary |
| Cutting | Edge marks may appear |
| CNC machining | Tool marks may remain |
| Deburring | Uneven edges may show |
| Brushing | Direction may not be consistent |
| Handling | Scratches may happen |
| Cleaning | Stains may remain |
| Anodizing | Defects become visible |
| Packing | Surface can still be scratched |
This is why highly visible parts need a different level of planning.
If an enclosure will sit on a customer’s desk, appear in product photos, or be sold as a premium device, visual details matter.
A small scratch on an internal mounting plate is nothing.
A small scratch on the top cover of a premium enclosure is a complaint waiting to happen.
Better Options for Decorative Products
For some cosmetic products, powder coating or painting may offer better appearance control.
They can cover small surface defects better. They also allow more stable color matching. Textured finishes can hide fingerprints, scratches, and small marks.
| Cosmetic Requirement | Better Option |
|---|---|
| Perfect brand color | Powder coating or painting |
| Hiding small surface marks | Textured powder coating |
| Matte black with stable appearance | Powder coating |
| Premium natural metal look | Anodizing with strict surface prep |
| High-gloss decorative surface | Painting or special coating |
| Logo and graphics | UV printing, silk screen, laser engraving |
This does not mean anodizing is bad for cosmetic products.
It means anodizing is honest.
It shows the surface you prepared.
For visible cosmetic parts, I do not only ask what color the customer wants. I check where the user’s eyes will land first, because that area needs more surface preparation than hidden walls or internal plates.
That is a small but important difference.
If the top cover is the face of the product, it deserves more attention than the bottom plate.
A customer may not notice a perfect internal bracket.
But they will notice one tiny scratch near the logo.
People judge products fast. Sometimes too fast. But that is how markets work.
Comparing Anodizing with Other Finishing Options
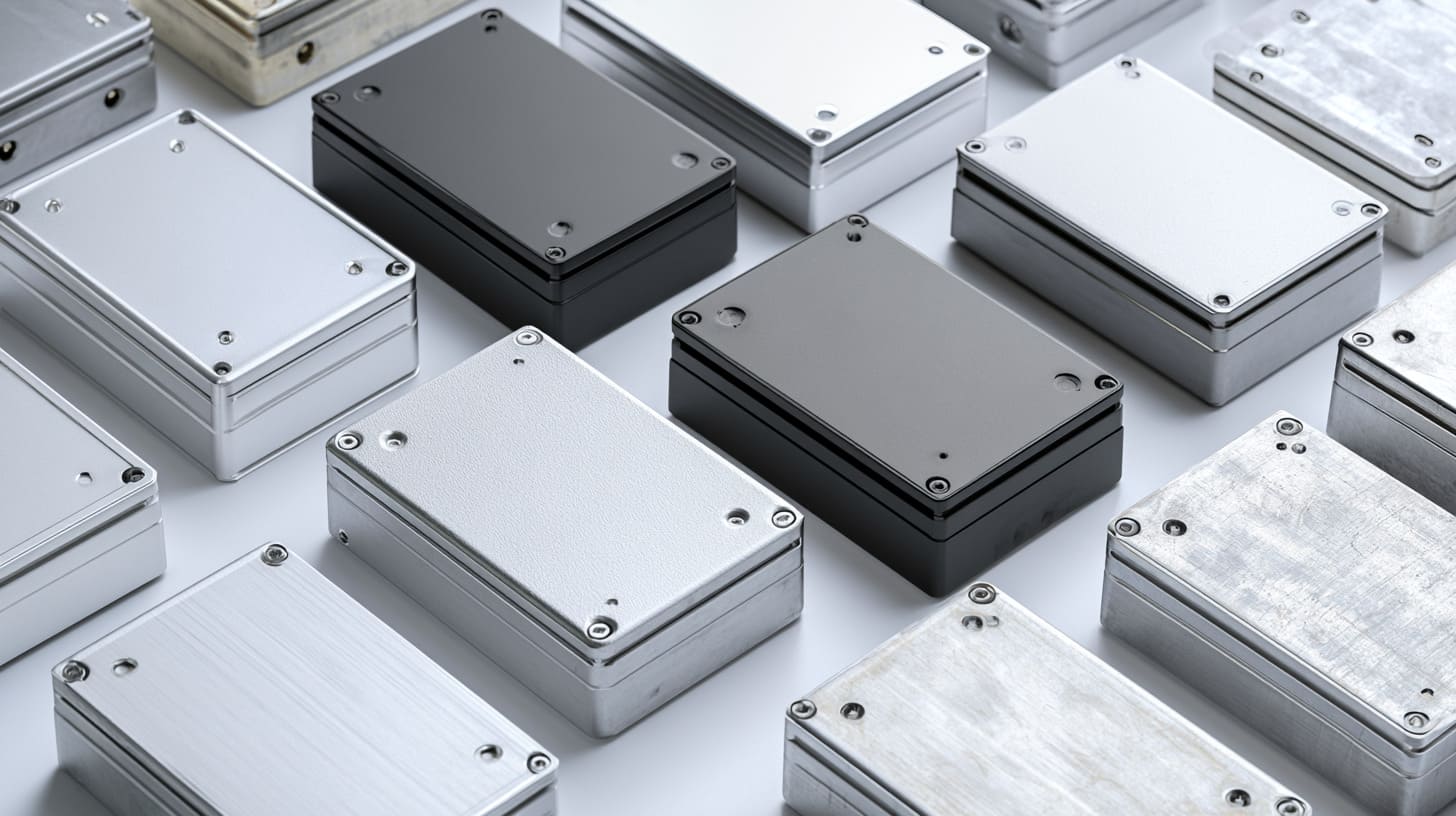
Choosing a finish is not about finding the “best” surface treatment.
It is about choosing the best fit for the job.
Anodizing, powder coating, painting, and bare aluminum all have strengths. They also have weaknesses. The wrong finish can make a good enclosure harder to assemble, harder to sell, or harder to control in production.
Anodizing vs Powder Coating
Powder coating is one of the most common alternatives to anodizing.
It uses dry powder that is applied to the metal and then cured with heat. It creates a thicker coating than anodizing.
| Factor | Anodizing | Powder Coating |
|---|---|---|
| Appearance | Metal texture remains | Coated appearance |
| Thickness | Thin | Thicker |
| Color consistency | Good, but variation possible | Usually better |
| Electrical conductivity | Insulating surface | Also insulating unless contact areas are managed |
| Scratch resistance | Good surface hardness | Good overall protection |
| Impact resistance | Can show edge damage | Often better for industrial use |
| Cost | Depends on batch and color | Often competitive |
| Tolerance impact | Small but important | Bigger because coating is thicker |
Anodizing feels more “metal.” Powder coating feels more “coated.”
If the customer wants a premium aluminum look, anodizing is attractive. If the customer wants strong color coverage and better hiding of surface defects, powder coating may be better.
Anodizing vs Painting
Painting gives more flexibility in color and finish.
It can be useful for products that need special brand colors, gloss levels, or decorative effects.
| Factor | Anodizing | Painting |
|---|---|---|
| Color flexibility | Limited compared with paint | Very flexible |
| Surface feel | Metal-like | Paint-like |
| Repairability | Harder to repair perfectly | Easier to touch up in some cases |
| Durability | Strong if used correctly | Depends on paint system |
| Cosmetic control | Surface defects may show | Can hide small defects better |
| Environmental resistance | Good | Depends on coating quality |
Painting can be a good choice for decorative products. But paint quality depends heavily on process control. Poor painting can chip, peel, or look uneven.
So I do not treat painting as a cheap magic solution.
It needs the right supplier and the right inspection standard.
Anodizing vs Bare Aluminum
Bare aluminum is the simplest option.
It is useful for prototypes, internal parts, or low-cost applications. But it has limits.
| Factor | Anodizing | Bare Aluminum |
|---|---|---|
| Cost | Higher | Lower |
| Corrosion resistance | Better | Lower |
| Appearance | Cleaner and more controlled | Raw and unfinished |
| Surface hardness | Better | Softer |
| Conductivity | Surface is insulating | Conductive |
| Prototype speed | Slower | Faster |
| Long-term use | Better | Depends on environment |
Bare aluminum may be enough for early testing. It may not be enough for final products.
The decision depends on how the enclosure will be used.
I choose finishes by thinking about the worst normal day of the product, not the best day in the sample room. If the enclosure will be touched, shipped, installed, scratched, cleaned, and re-ordered, the finish must survive that real life, not just the first photo.
That is the difference between a surface that looks good once and a surface that works for the customer.
How to Decide Whether Anodizing Is Right for Your Aluminum Enclosure
A good finish decision starts before production.
It should not be left until the last day.
When a customer sends me an enclosure design, I prefer to talk about the finish together with the structure. The finish affects cost, tolerance, grounding, appearance, lead time, packaging, and even how the customer uses the product.
Questions to Ask Before Selecting a Finish
Here are the questions I like to ask before recommending anodizing:
| Question | Why I Ask It |
|---|---|
| Where will the enclosure be used? | Indoor and outdoor use need different protection |
| Will the surface be touched often? | Frequent handling affects scratch and fingerprint control |
| Does the enclosure need grounding? | Anodizing may block electrical contact |
| Are there tight threads or sliding parts? | Surface buildup may affect assembly |
| Does the color need to match future orders? | Anodizing may have batch variation |
| Is this a prototype or final production? | Early prototypes may not need anodizing |
| Is the enclosure visible to end users? | Cosmetic standards may need stricter control |
| What is the target budget? | Some finishes may not match the cost goal |
| How fast does the customer need delivery? | Finishing can affect lead time |
| Will the product be used in harsh conditions? | Impact and wear resistance matter |
These questions may look simple. But they prevent many problems.
For example, if a customer says the enclosure is for indoor use and hidden inside another machine, maybe anodizing is not needed.
If the customer says the enclosure is part of a premium desktop product, anodizing may be useful.
If the customer says the enclosure needs grounding and EMI shielding, anodizing must be planned with masked contact areas.
If the customer says the first batch is only for testing, maybe we should wait before final anodizing.
Working with an Experienced Enclosure Manufacturer
A good manufacturer should not only follow the drawing blindly.
Of course, the drawing is important. But if I see a possible issue, I should speak up.
That is part of the value of custom manufacturing.
For aluminum enclosures, the finish should be discussed together with:
- Material grade
- Wall thickness
- CNC or sheet metal process
- Hole tolerance
- Thread position
- Assembly method
- PCB mounting
- Grounding points
- Logo method
- Packaging method
- Expected usage environment
Here is a practical decision table:
| If Your Main Priority Is... | Consider This Finish |
|---|---|
| Premium metal appearance | Anodizing |
| Stable brand color | Powder coating or painting |
| Electrical grounding | Bare contact areas or conductive treatment |
| Fast prototype | Raw aluminum or simple brushed finish |
| Harsh industrial use | Powder coating or hybrid protection |
| Low-cost internal part | Raw or simple finish |
| High cosmetic standard | Anodizing with strict prep, or powder coating |
| Long-term outdoor use | Anodizing, powder coating, or special coating based on environment |
One thing I always try to understand is the customer’s real risk. Sometimes the biggest risk is not corrosion. It is missed delivery. Sometimes it is not cost. It is poor grounding. Sometimes it is not color. It is customer complaints after the second batch.
That is why I do not like one-size-fits-all answers.
For me, anodizing is a tool.
A useful tool.
But still just a tool.
A hammer is useful too. But I will not use it to tighten a screw.
Conclusion
I like anodizing.
I recommend it often for custom aluminum enclosures because it can give a clean appearance, better corrosion resistance, improved surface hardness, and a professional metal finish.
But I do not recommend it blindly.
I have worked with enough enclosure projects to know that the wrong finish can create problems that are easy to avoid. A product may look better with anodizing, but it may cost more than needed. It may lose electrical contact. It may create assembly trouble. It may show color variation. It may delay prototype testing. It may also highlight surface defects that powder coating could hide.
This is why I judge anodizing from the real application, not from the finish name.
If the enclosure needs a premium metal look, anodizing may be the right choice.
If the enclosure needs grounding, tight fit, perfect color matching, low cost, fast prototype speed, or heavy impact resistance, I will slow down and check other options first.
My experience tells me that a good enclosure is not only about the material. It is not only about CNC machining. It is not only about a nice black surface.
A good enclosure is a balance.
It must protect the customer’s electronics. It must fit the PCB. It must support assembly. It must meet the budget. It must arrive on time. It must look right for the market. It must not create hidden problems after production.
That is why I think surface finish selection should happen early, not at the end.
At MaidaTech, we produce custom aluminum enclosures, plastic enclosures, sheet metal enclosures, and OEM/ODM enclosure solutions for B2B customers. If you already have a drawing, we can help review the structure, surface finish, logo method, packaging, and production plan before mass production.
If you are not sure whether anodizing is right for your aluminum enclosure, you can send us your drawing, quantity, application, and surface requirement.
I will not simply say “yes, anodizing is good.”
I will help you check whether it is truly the right choice for your project.