Skip to content
When a powder-coated steel enclosure begins to blister at a weld or rust at a lower seam, the visible coating is often blamed first. In many cases, the real problem started before the spray booth: oil remained on the steel, a weld was not cleaned properly, flash rust developed after washing, or the selected conversion treatment did not match the material and service conditions.
Steel pretreatment before powder coating is the controlled work that makes the metal clean, chemically ready, and stable enough for the coating system to bond and protect. For a custom enclosure, it is not simply a quick wash. It connects fabrication, cleaning, rinsing, conversion coating, drying, handling, powder application, and eventual installation.
In my factory work, I treat pretreatment as a quality decision made alongside the drawing and finish specification. That is where we prevent a good-looking color sample from becoming a costly field complaint.
The useful starting point is to understand what this stage must accomplish before choosing a process name.
What Steel Pretreatment Must Accomplish
Remove the contamination that powder cannot hide
Steel enclosure parts can pick up cutting fluid, press lubricant, weld residue, grinding dust, shop dirt, fingerprints, oxide, salts, and handling contamination before they reach the coating line. Powder coating has no solvent phase to forgive a poorly cleaned surface. The Powder Coating Institute makes this point clearly: cleaning quality, pretreatment selection, and cure all affect whether the coating adheres as intended.
The correct cleaning route depends on the steel, the soil, contact time, bath conditions, process equipment, and environmental controls. A part that arrives from laser cutting may need a different focus from a part that has been stored outdoors, welded heavily, or handled with forming lubricant.
Create a coating-ready interface
After cleaning, a qualified conversion treatment can give the coating system a more stable surface to bond to and can support under-film corrosion resistance. The U.S. EPA’s coating-industry manual describes phosphating as a conversion coating used on steel and galvanized steel before powder, liquid, or electrodeposited coatings.
I do not describe that conversion layer as a substitute for a powder coat, a gasket, or good drainage. It is one layer of a protection system, and its value is lost if the steel returns to contamination before application.
That is why the next step is not choosing a bath by habit; it is identifying exactly what steel and fabrication condition will enter the line.
Start With the Steel and Fabrication Route
“Steel” is not one starting condition
Cold-rolled steel, hot-rolled steel, galvanized steel, parts with a shop primer, and previously coated parts can require different preparation decisions. Mill scale, oxide, galvanizing condition, surface profile, old coating, and storage history can change what cleaning or mechanical preparation is appropriate. ISO 12944-4 recognizes this breadth by covering uncoated, galvanized, zinc-electroplated, thermally sprayed, and previously painted steel surfaces.
A buyer does not need to prescribe the entire wash-line chemistry without knowing the supplier’s qualified system. But the RFQ should identify the substrate and its prior condition. That lets the supplier determine whether cleaning alone is adequate or whether mechanical preparation, a particular conversion route, or a separate qualification is needed.
Welds and cut edges deserve their own review
Spatter, burrs, porous welds, sharp corners, grinding debris, and trapped process residue are not small cosmetic issues. They can be difficult to clean and coat, and they create locations where a film may be thin or where moisture can sit later. A smooth, accessible weld and a practical edge break make the whole process more repeatable.
I would rather correct a burr or an inaccessible seam before the first article than try to rescue it with a thicker-looking finish. Extra powder does not make an unclean crevice or a razor edge behave like a well-prepared surface.
Once the incoming part is defined, the treatment sequence can be reviewed as a controlled chain rather than a black box.
The Typical Pretreatment Sequence
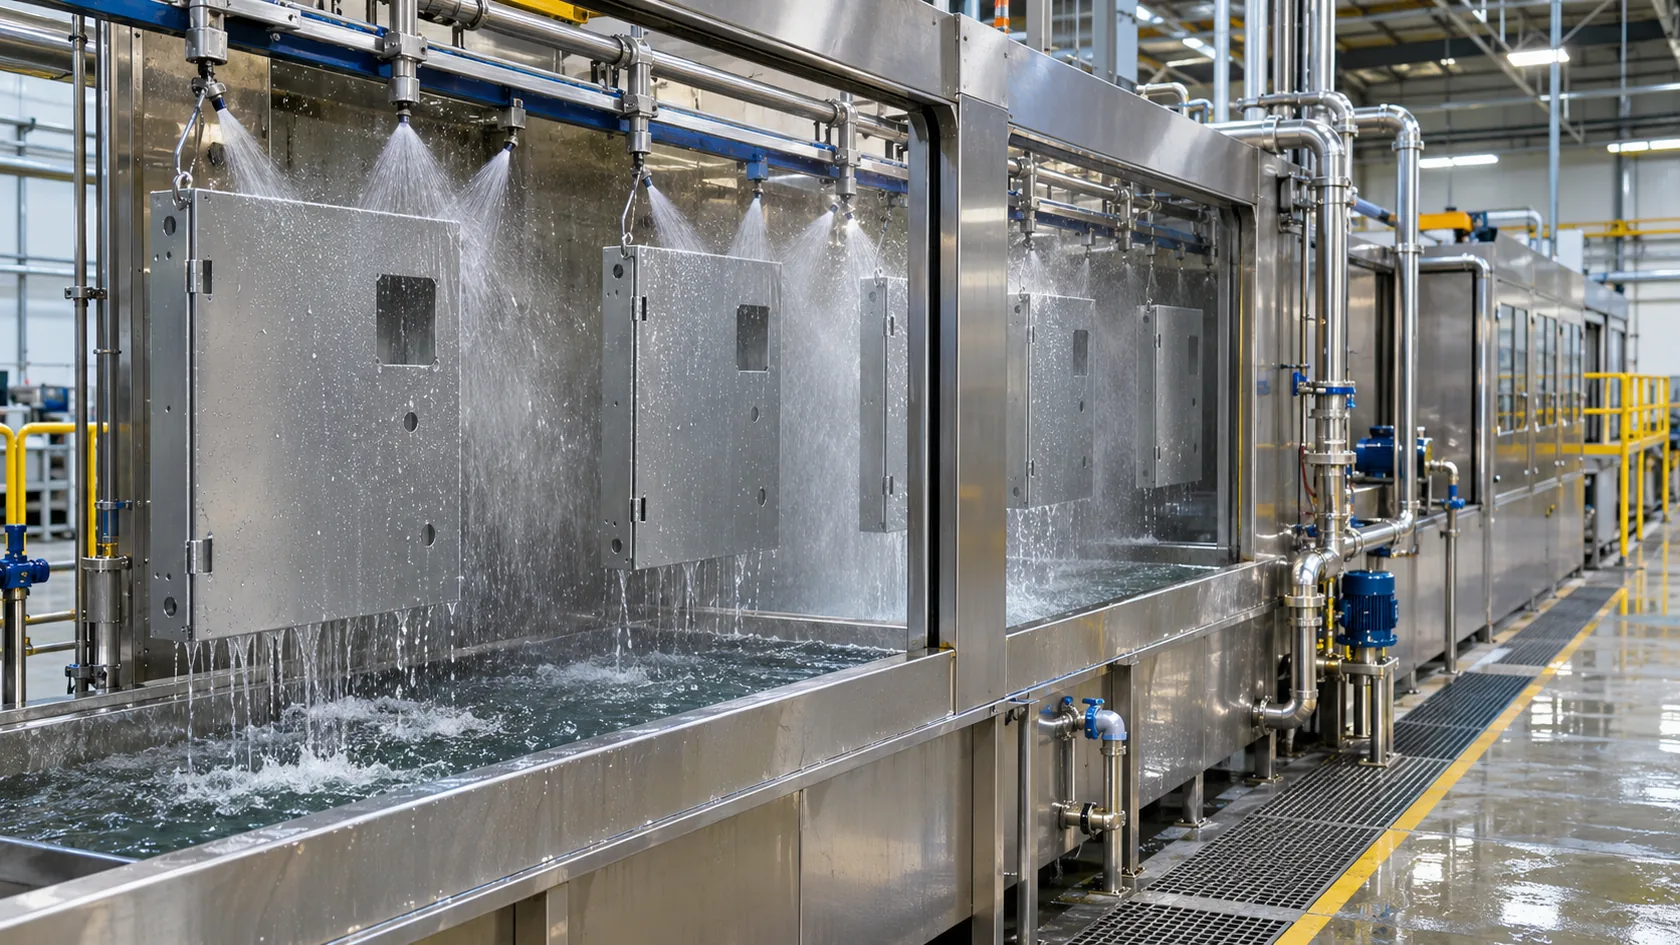
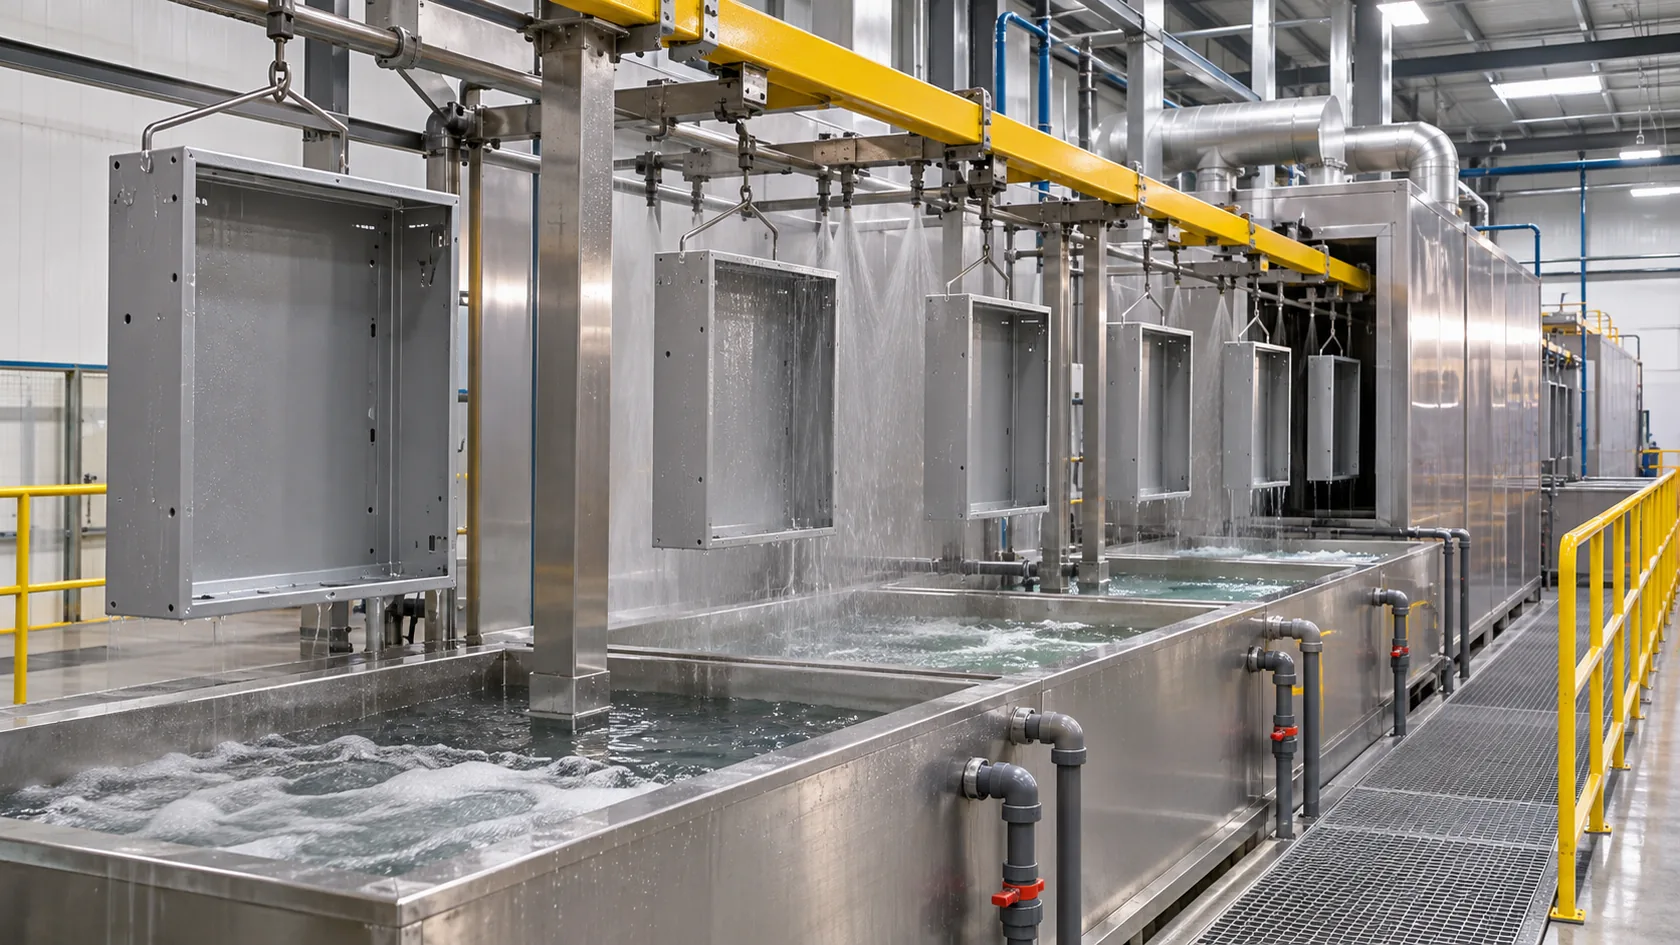
Cleaning, rinsing, conversion, drying
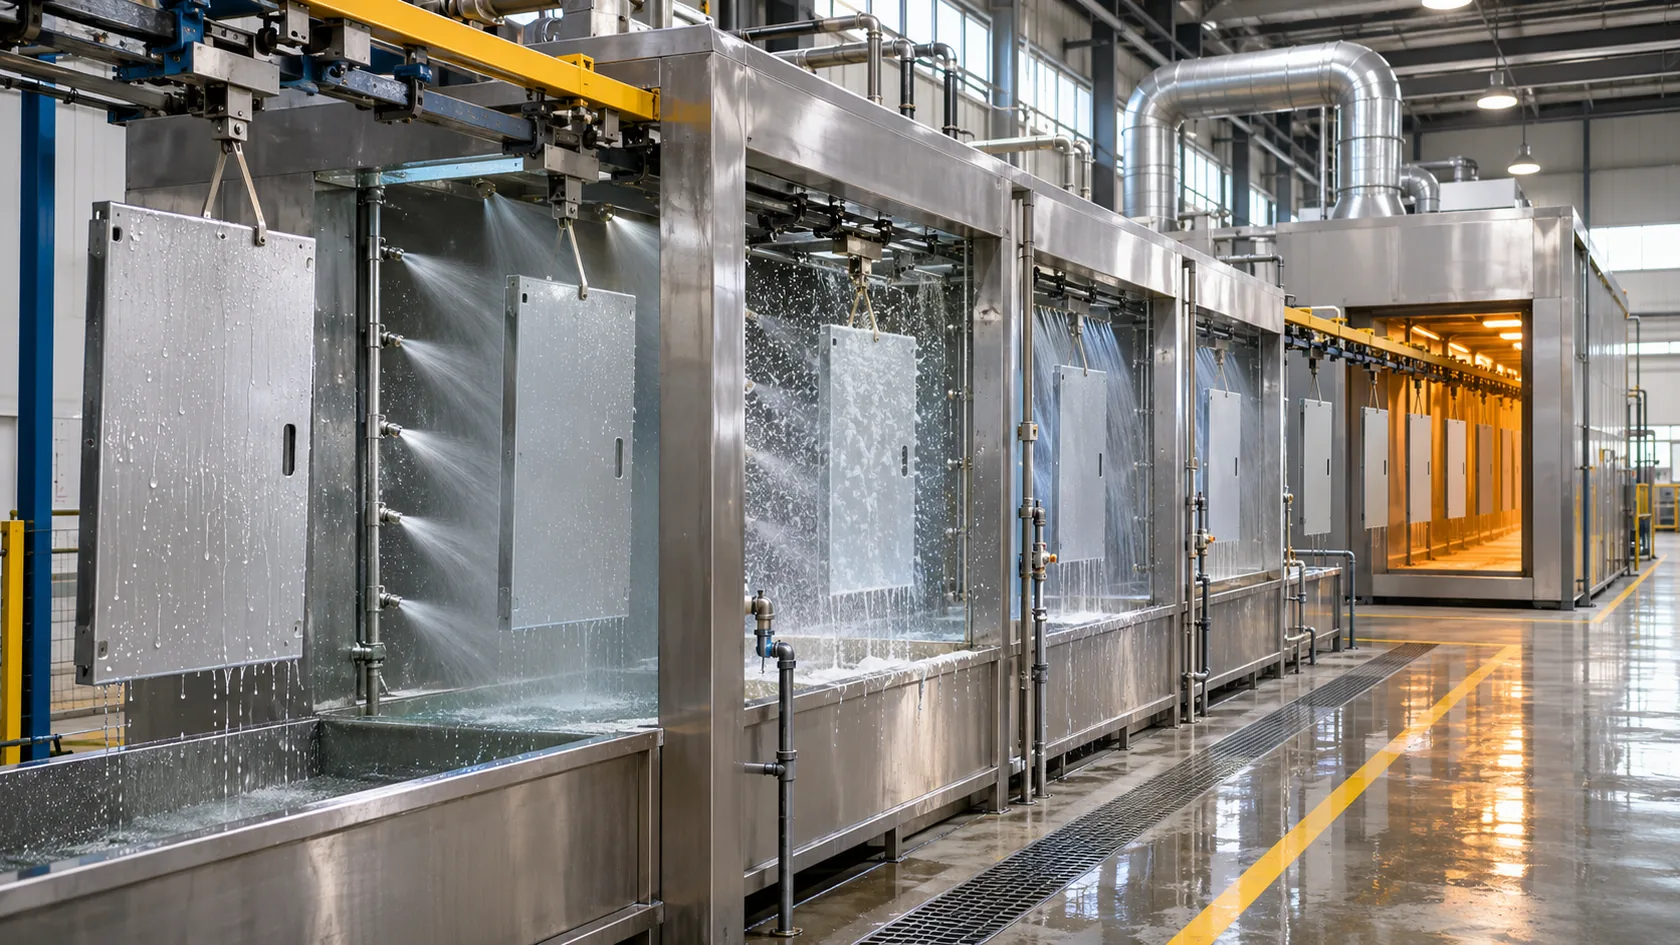
A production sequence commonly includes cleaning to remove soils, rinsing to avoid carrying cleaner into later stages, a conversion treatment, further rinsing or sealing as appropriate to the qualified process, and drying before powder application. The actual number of stages and chemistry are supplier- and system-specific. It is not sound engineering to assume every “five-stage” or “seven-stage” line gives the same result.
The important point is that each stage must do its assigned job without damaging the next one. Carry-over, exhausted chemistry, poor rinse quality, insufficient dwell time, or inadequate drying can reduce the value of the whole sequence. A clean-looking part is not necessarily a process-confirmed part.
Keep the handoff to the powder booth clean
After final treatment, parts still need controlled racking, handling, staging, and timing. Dirty hooks, bare hands, condensation, dust, or an extended queue can reintroduce risk. I pay particular attention to complex enclosures because doors, bodies, and mounting plates may travel through the line at different times and must still finish as a compatible system.
| Stage | Main purpose | Buyer or engineer check |
|---|---|---|
| Fabrication cleanup | Remove burrs, spatter, residue, and inaccessible traps | Are welds and edges accepted before wash-line entry? |
| Cleaning and rinse | Remove oils, salts, and shop contamination | Does the cleaning process match the part’s actual soils? |
| Conversion treatment | Prepare a qualified bonding and corrosion-control interface | Is the process compatible with the material and powder system? |
| Drying and handling | Prevent moisture and recontamination before coating | How are parts racked, stored, and protected before spraying? |
That controlled sequence gives a conversion coating its real meaning, which is different from treating every phosphate process as interchangeable.
Conversion Coatings Are a System Decision
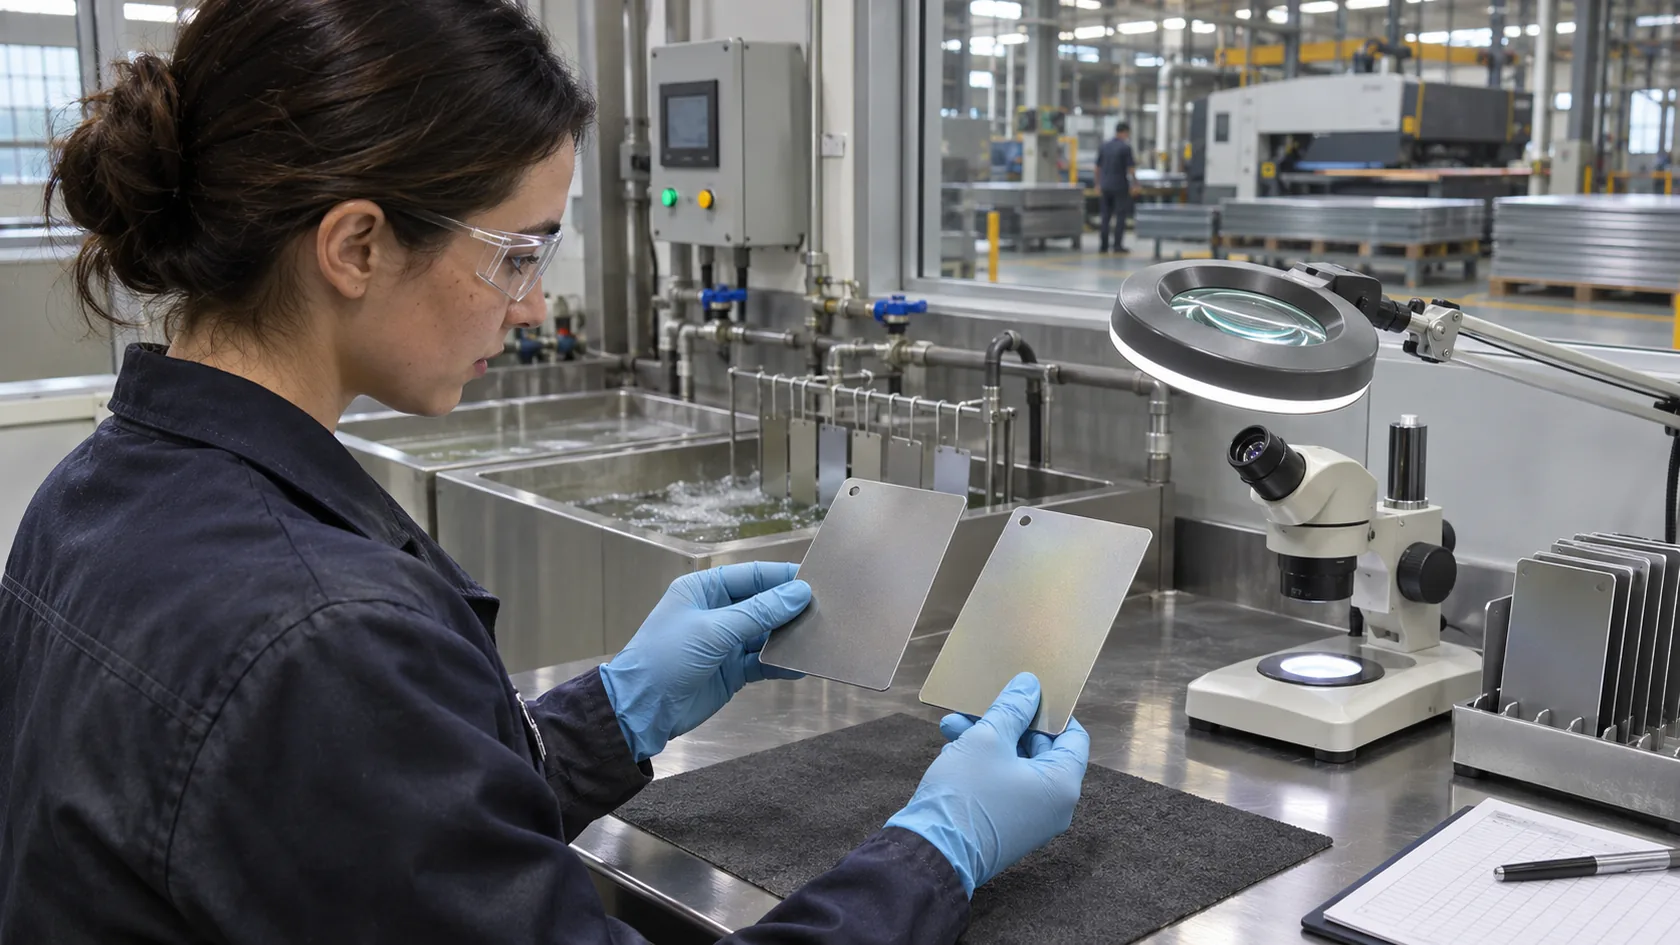
Iron phosphate and zinc phosphate have different contexts
The Powder Coating Institute identifies iron phosphate as the most frequently used powder-coating pretreatment and notes that zinc phosphate can be appropriate when a higher performance level is needed. Neither name is a guarantee by itself. The released powder product, steel condition, fabrication geometry, line controls, expected exposure, and acceptance plan determine whether the system is suitable.
For a modest indoor enclosure, a supplier’s qualified standard process may be the practical choice. For an outdoor enclosure with higher corrosion exposure, the pretreatment question should be reviewed together with powder chemistry, seams, cut edges, drainage, hardware, and validation. A request for “zinc phosphate” without those details can still leave too much ambiguity.
Galvanized components need compatible preparation
Galvanized steel is not simply bare steel with better corrosion resistance. The American Galvanizers Association explains that surface preparation is critical before powder coating hot-dip galvanized steel and identifies profiling methods such as sweep blasting, zinc-phosphate treatment, or surface grinding for appropriate cases.
My advice is to tell the coating supplier when a design mixes bare and galvanized steel, or when galvanizing is planned after fabrication. The stack-up, weld details, mechanical preparation, and powder system all deserve a compatibility check before production begins.
The chemistry choice only succeeds when the enclosure geometry allows those controlled processes to reach the places that matter.
Enclosure Geometry Can Undermine a Good Wash Line
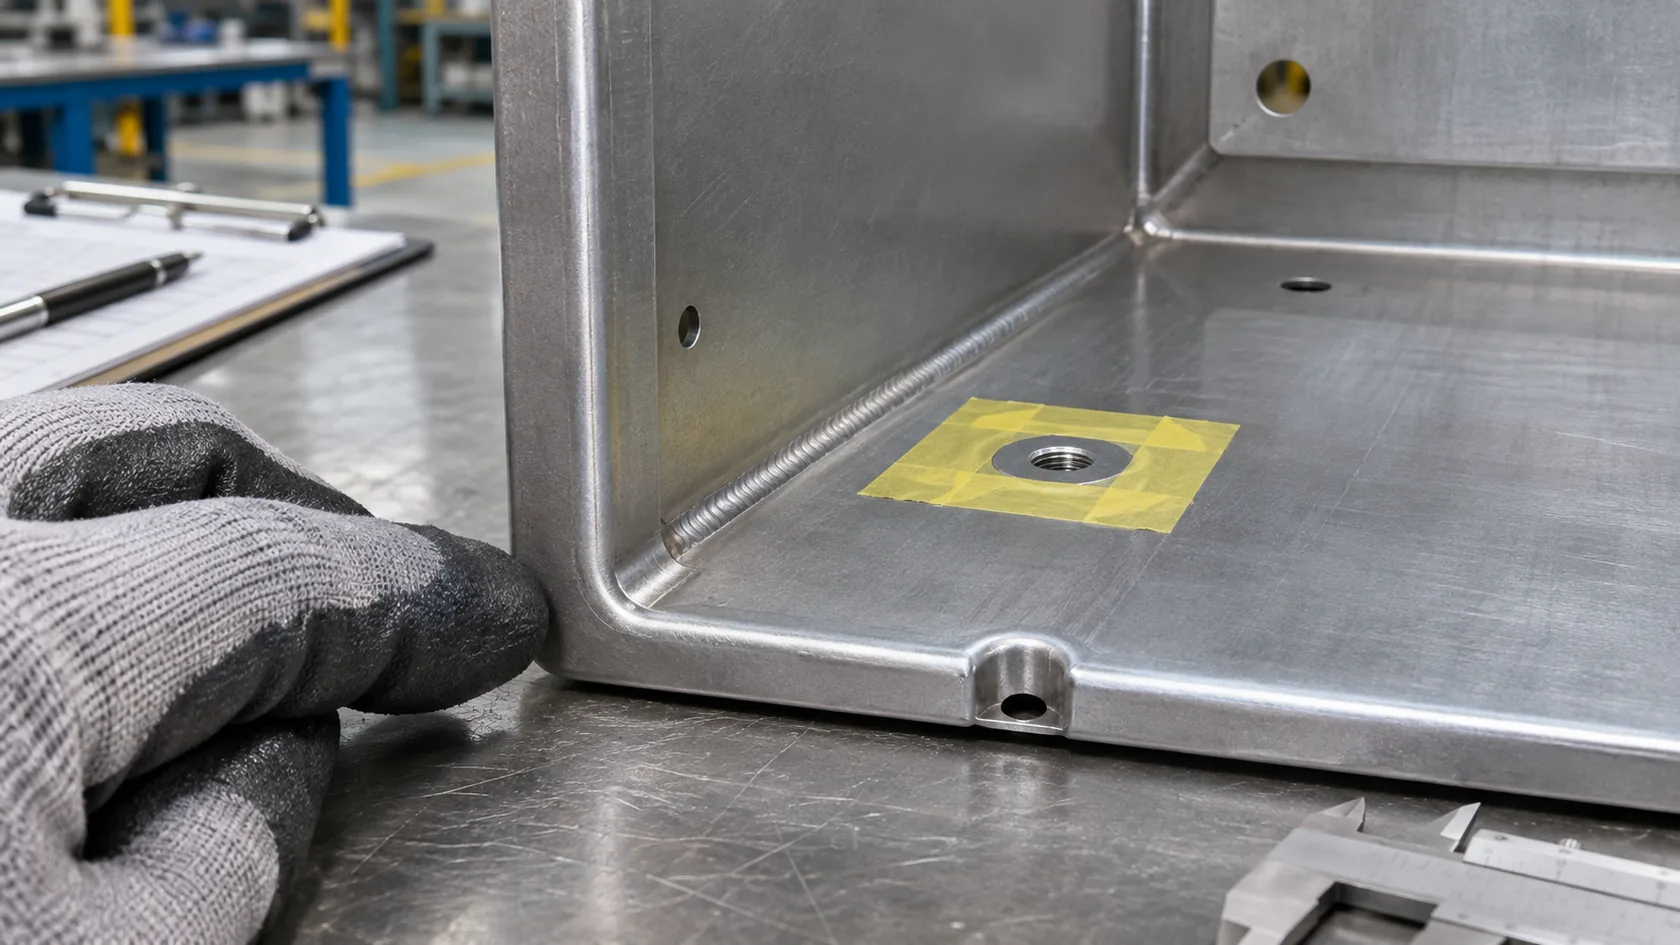
Design for cleaning, coating, drainage, and inspection
Deep return flanges, narrow gaps, overlapped panels, blind corners, porous welds, tightly closed seams, and horizontal pockets can be difficult to clean, rinse, dry, coat, or inspect. After installation, those same features may hold rain, condensation, or cleaning water. ISO 12944-3 addresses design criteria that help prevent premature corrosion and enable coating application, inspection, and maintenance.
For an enclosure, I review the lower door edge, roof features, rear mounting interface, cable-entry region, bracket contact, and any folded seam. Water paths are often more revealing than the broad visible face. If a detail cannot drain or dry, the nominal outdoor condition at that location may be much harsher than the project description suggests.
Keep electrical interfaces intentional
Powder coating is normally insulating. A grounding or EMC contact should not be created by casually scratching away paint after assembly. If a conductive land, stud, gasket interface, or hardware contact is needed, define the mask, contact method, assembly protection, and corrosion plan together. The same care applies to holes drilled after coating: a post-coat change can expose steel and defeat an otherwise sound pretreatment system.
In my experience, the best time to resolve a conductive contact or drainage detail is before the first treated part reaches the booth. It is faster, cheaper, and much easier to validate.
With the part and process aligned, the final task is to test evidence that reflects the actual part rather than a generic claim.
Confirm the Coating on the Real Part
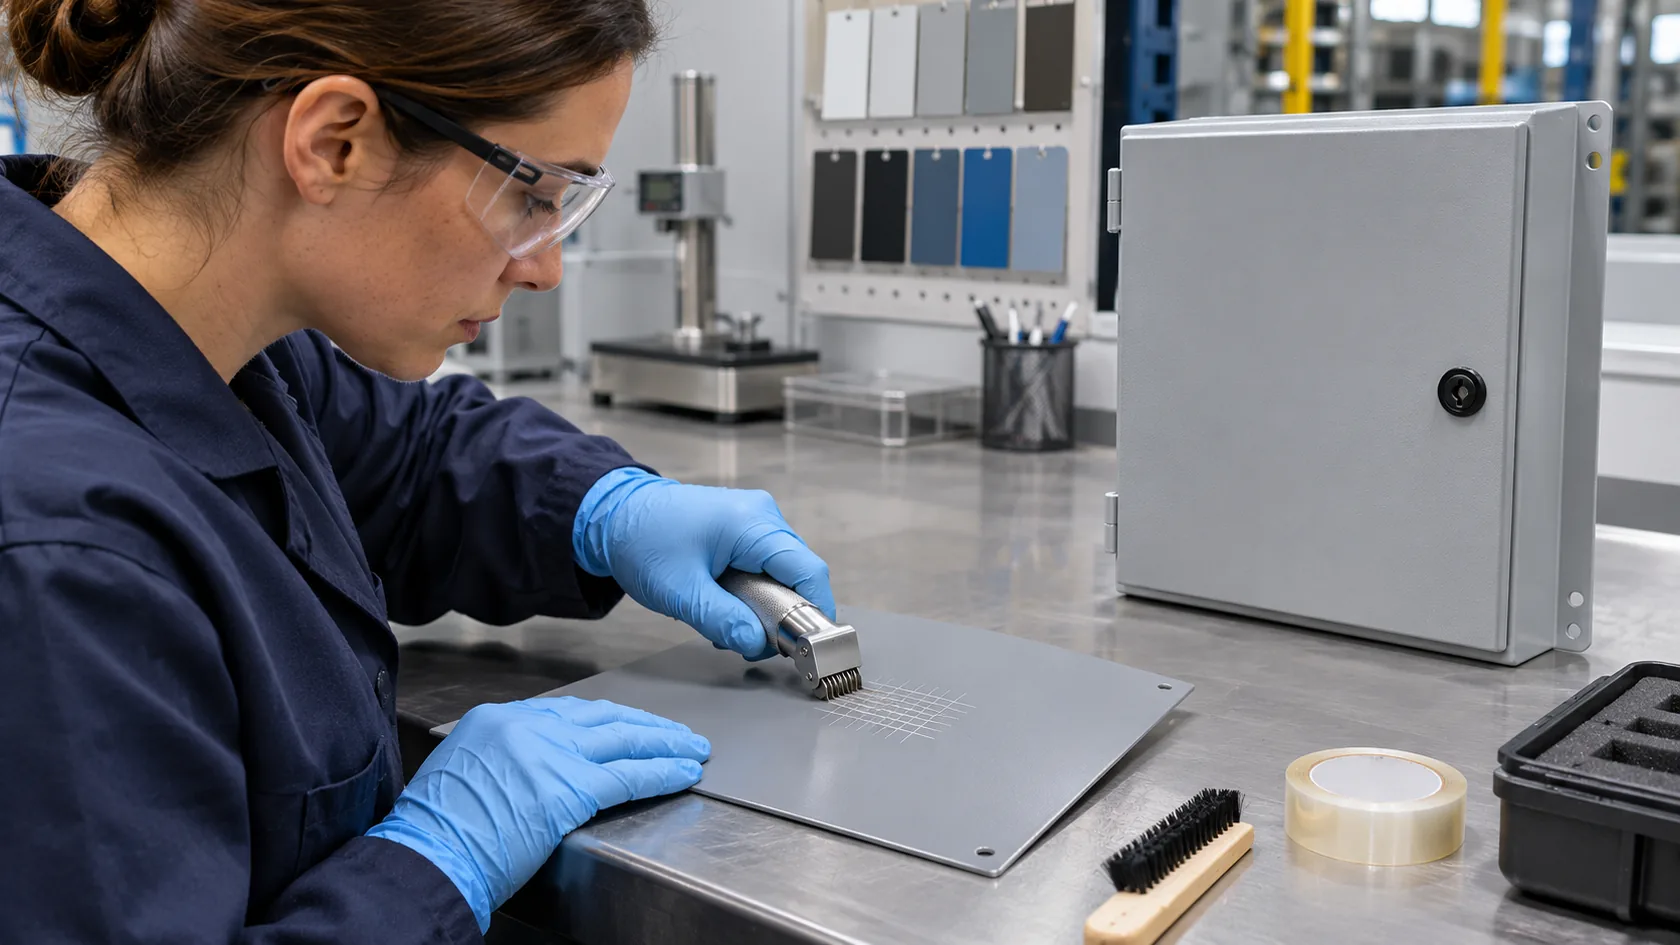
Approve a representative first article
The first article should use representative substrate, fabrication, pretreatment, powder product, color or texture, racking, and cure process. Check broad faces, but also inspect accessible recesses, edges, weld areas, masking zones, and assembly interfaces. A flat coupon is useful for process control; it cannot fully demonstrate coverage and drainage on a complex cabinet.
The powder supplier’s cure schedule also needs to be applied through a process that heats the real part appropriately. A thin door, a heavy welded body, and a densely loaded rack can respond differently. Oven setpoint alone is not proof of the part’s cure condition.
Name the test and the pass criteria
ASTM D3359 provides tape-test methods for assessing adhesion on metallic substrates and emphasizes that surface preparation has a major effect on adhesion. It is useful when the agreed method, sample condition, test location, and acceptance result are stated in advance. It is not a universal substitute for evaluating corrosion protection or outdoor weathering.
If corrosion testing is requested, name the system, specimen or complete assembly, exposure, any scribe condition, duration, evaluation rule, and approval owner. ASTM B117 cautions that natural-environment correlation is seldom predictable when salt-spray results are used alone. Testing becomes useful when it answers a specific release question rather than supplying an impressive number for a brochure.
| Evidence | What it can help confirm | What it cannot prove alone |
|---|---|---|
| Visual and coverage inspection | Obvious defects, missed areas, and assembly damage | Long-term outdoor durability |
| Adhesion evaluation | Whether the coating bond meets the agreed screening method | Full corrosion performance of every detail |
| Controlled corrosion exposure | Comparative performance of a stated system and specimen | Exact field life in every climate |
| Installed assembly review | Water paths, cable entries, hardware, and conductive interfaces | Coating-process consistency without factory evidence |
This evidence is most useful when the buyer turns it into a concise RFQ release basis instead of treating pretreatment as a supplier mystery.
What Buyers Should Put in the RFQ
Make the process quotable and reviewable
An effective RFQ lets the sheet-metal team, coater, assembler, and inspector work from the same picture. It need not lock a supplier into a chemistry before technical review, but it should make the service conditions and critical details visible.
- Steel type, thickness range, and condition: cold-rolled, hot-rolled, galvanized, previously coated, or mixed.
- Fabrication details: edge condition, weld cleanup, overlaps, sealed or drainable seams, and inaccessible areas.
- Service environment: indoor or outdoor exposure, sun, salt, pollutants, chemicals, wetting, temperature cycling, and maintenance access.
- Finish target: approved powder system or approval route, color, gloss or texture, special masking, and appearance acceptance.
- Enclosure interfaces: cable entries, gaskets, vents, conductive contacts, hardware, mounting orientation, and post-coat operations.
- Release evidence: first-article checkpoints, agreed adhesion or corrosion methods when justified, records, and acceptance owner.
I find that this short checklist prevents far more confusion than a generic instruction to provide “heavy-duty pretreatment.” It gives the factory room to use a qualified process while protecting the buyer from an unreviewed substitution.
Pretreatment is therefore not a hidden back-room step; it is part of the technical agreement for the enclosure you expect to receive.
Conclusion
Steel pretreatment before powder coating is the controlled preparation that removes fabrication contamination, creates a compatible surface for the selected coating system, and protects the process against recontamination before application. For an enclosure, its value depends on the steel condition, welds and edges, pretreatment route, powder chemistry, cure, drainage, assembly details, and the real service environment.
After years of working through enclosure production details, I have learned that the small hidden areas deserve the first questions: a welded corner, a lower seam, a bracket contact, a masked earth point, or a place water can remain. Send us the drawing, steel condition, finish target, mounting direction, and exposure notes. We can review whether the pretreatment and coating plan support the enclosure before it enters production.